

Design and manufacture of press tools and moulds
We design and build progressive, tandem and transfer press tools, injection moulds, inspection fixtures and precision machined parts.
From the tool design stage onwards, we take into account functionality, service life, efficient use of material and the economics of subsequent production. We apply our experience in the automotive industry and other sectors.
- max. tool length
- 5 000 mm
- max. tool weight
- 30 t
From press tool to precision machined part
We use ROSTRA Tools' design and manufacturing experience to make press tools, injection moulds, precision machined parts and special fixtures. Our manufacturing capabilities are available to customers in the automotive industry and other sectors.
-
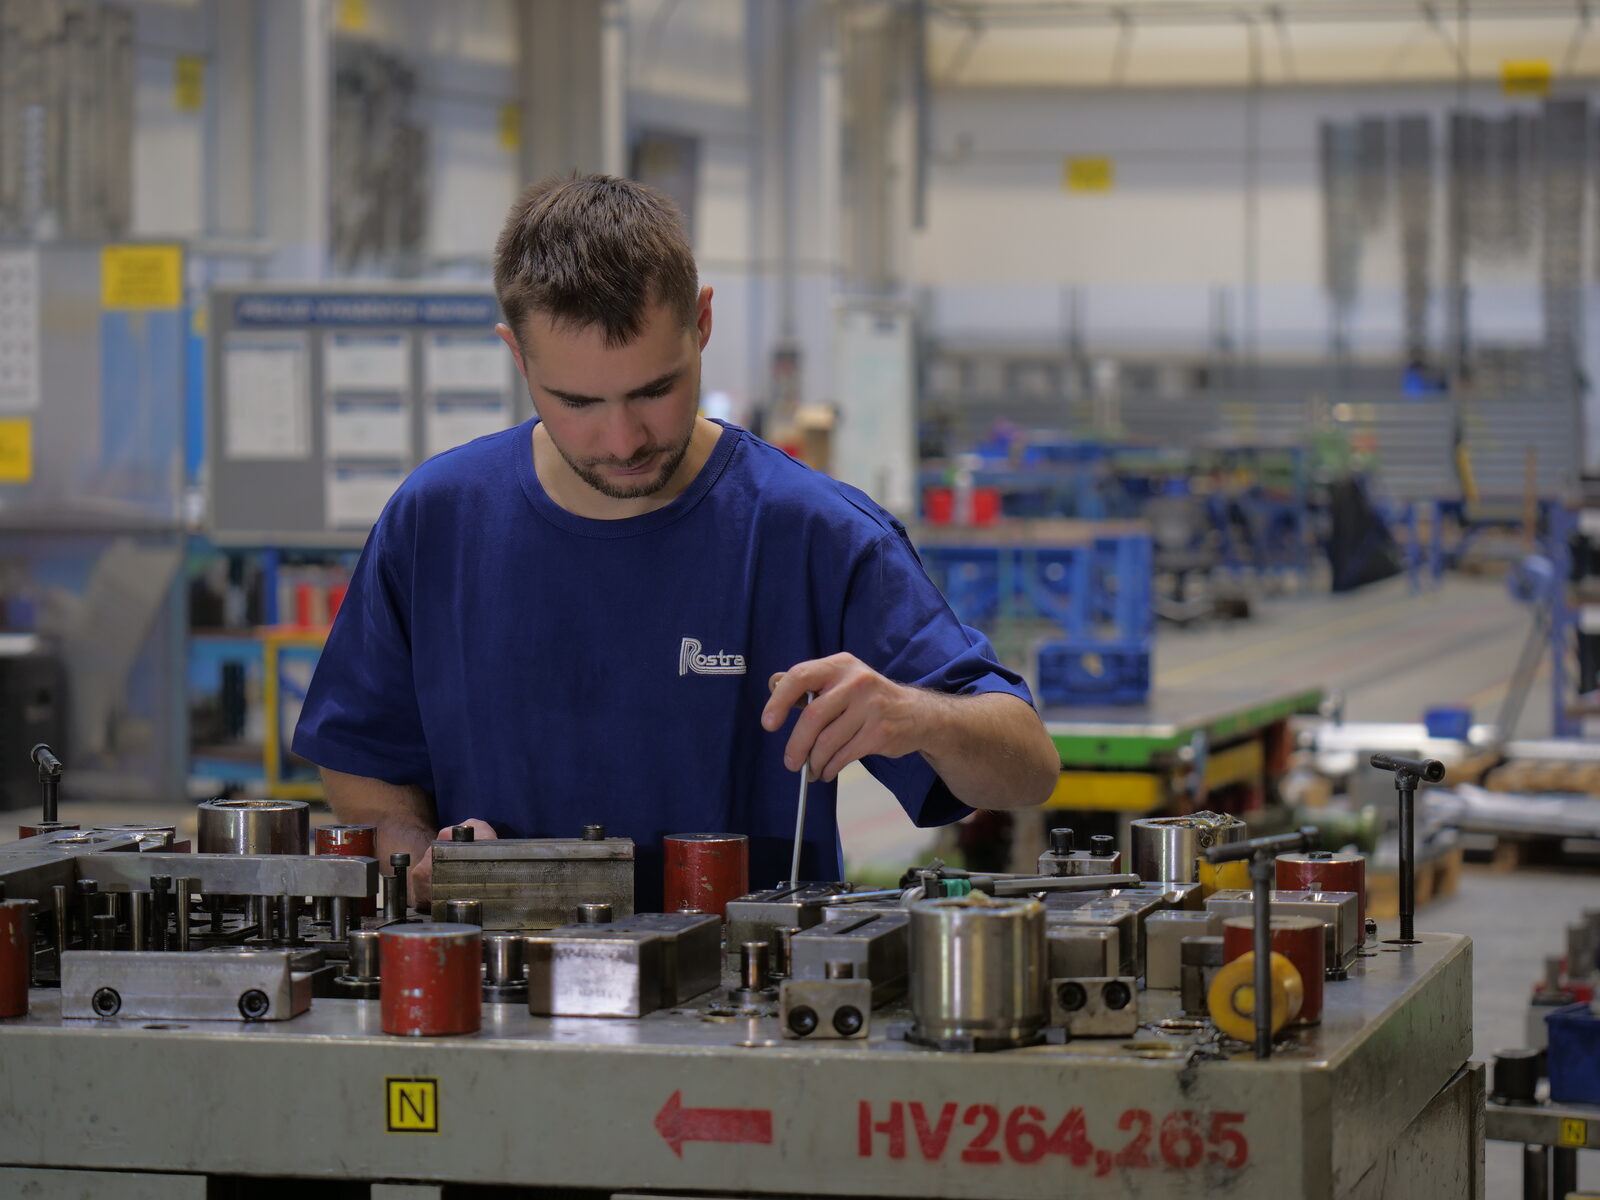
Press tools
We design and build progressive, tandem and transfer press tools for producing sheet-metal parts.
In the design we take into account the required precision, functionality and tool life, as well as efficient use of material in subsequent production.
-
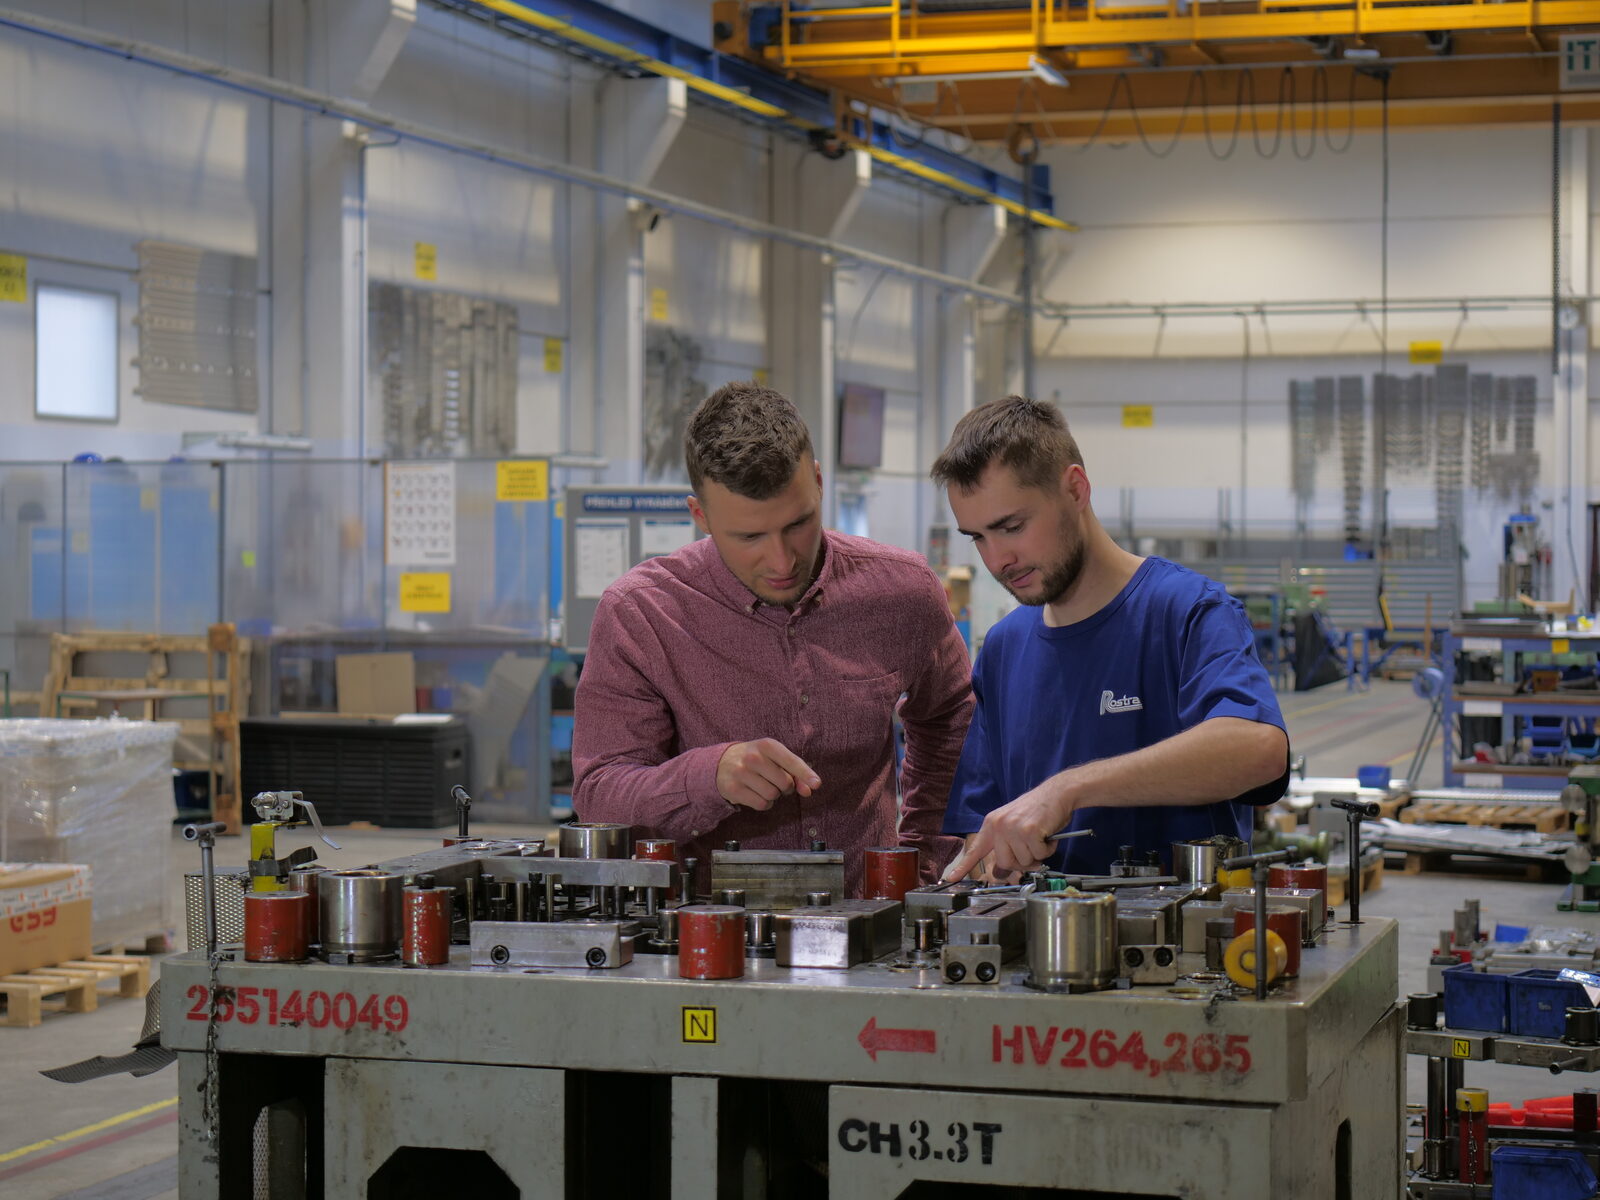
Injection moulds
We design and build moulds for injection moulding of plastic parts to the customer's technical requirements.
We provide the design, manufacture, assembly and finishing of moulds.
-
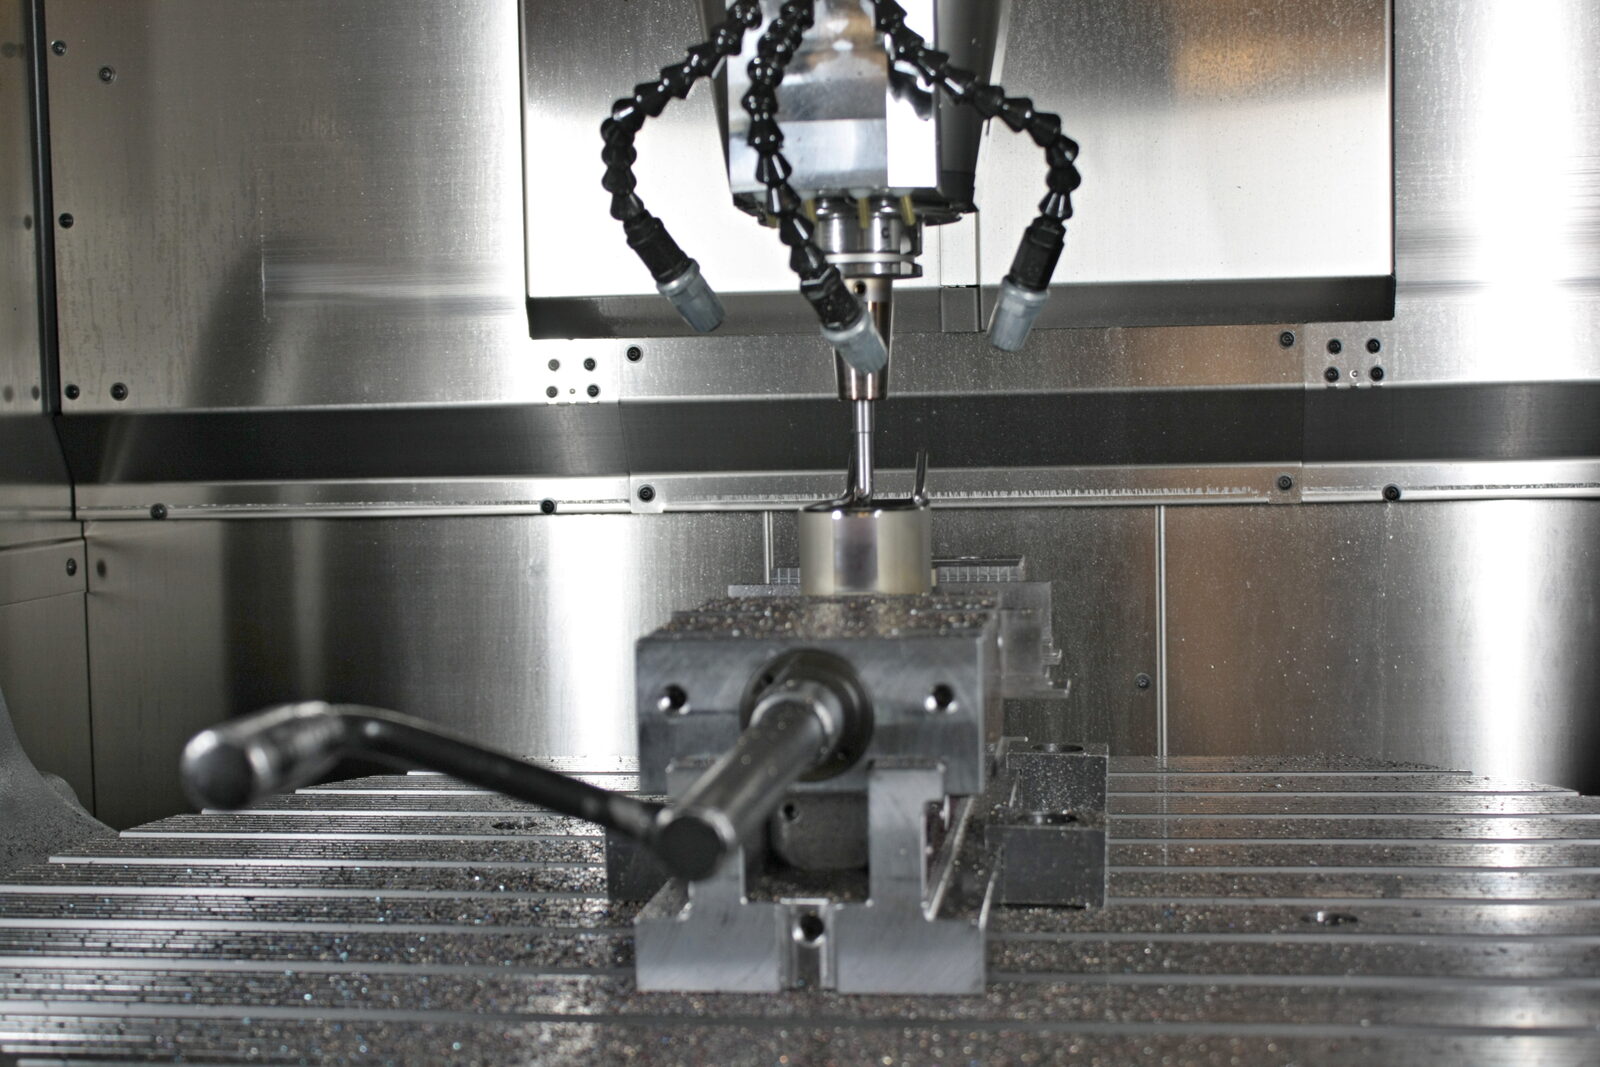
Precision machined parts
We produce custom machined parts from supplied drawings or 3D models.
We use CNC milling, wire and die-sinking EDM, and grinding. We also produce parts for press tools and other engineering applications.
-
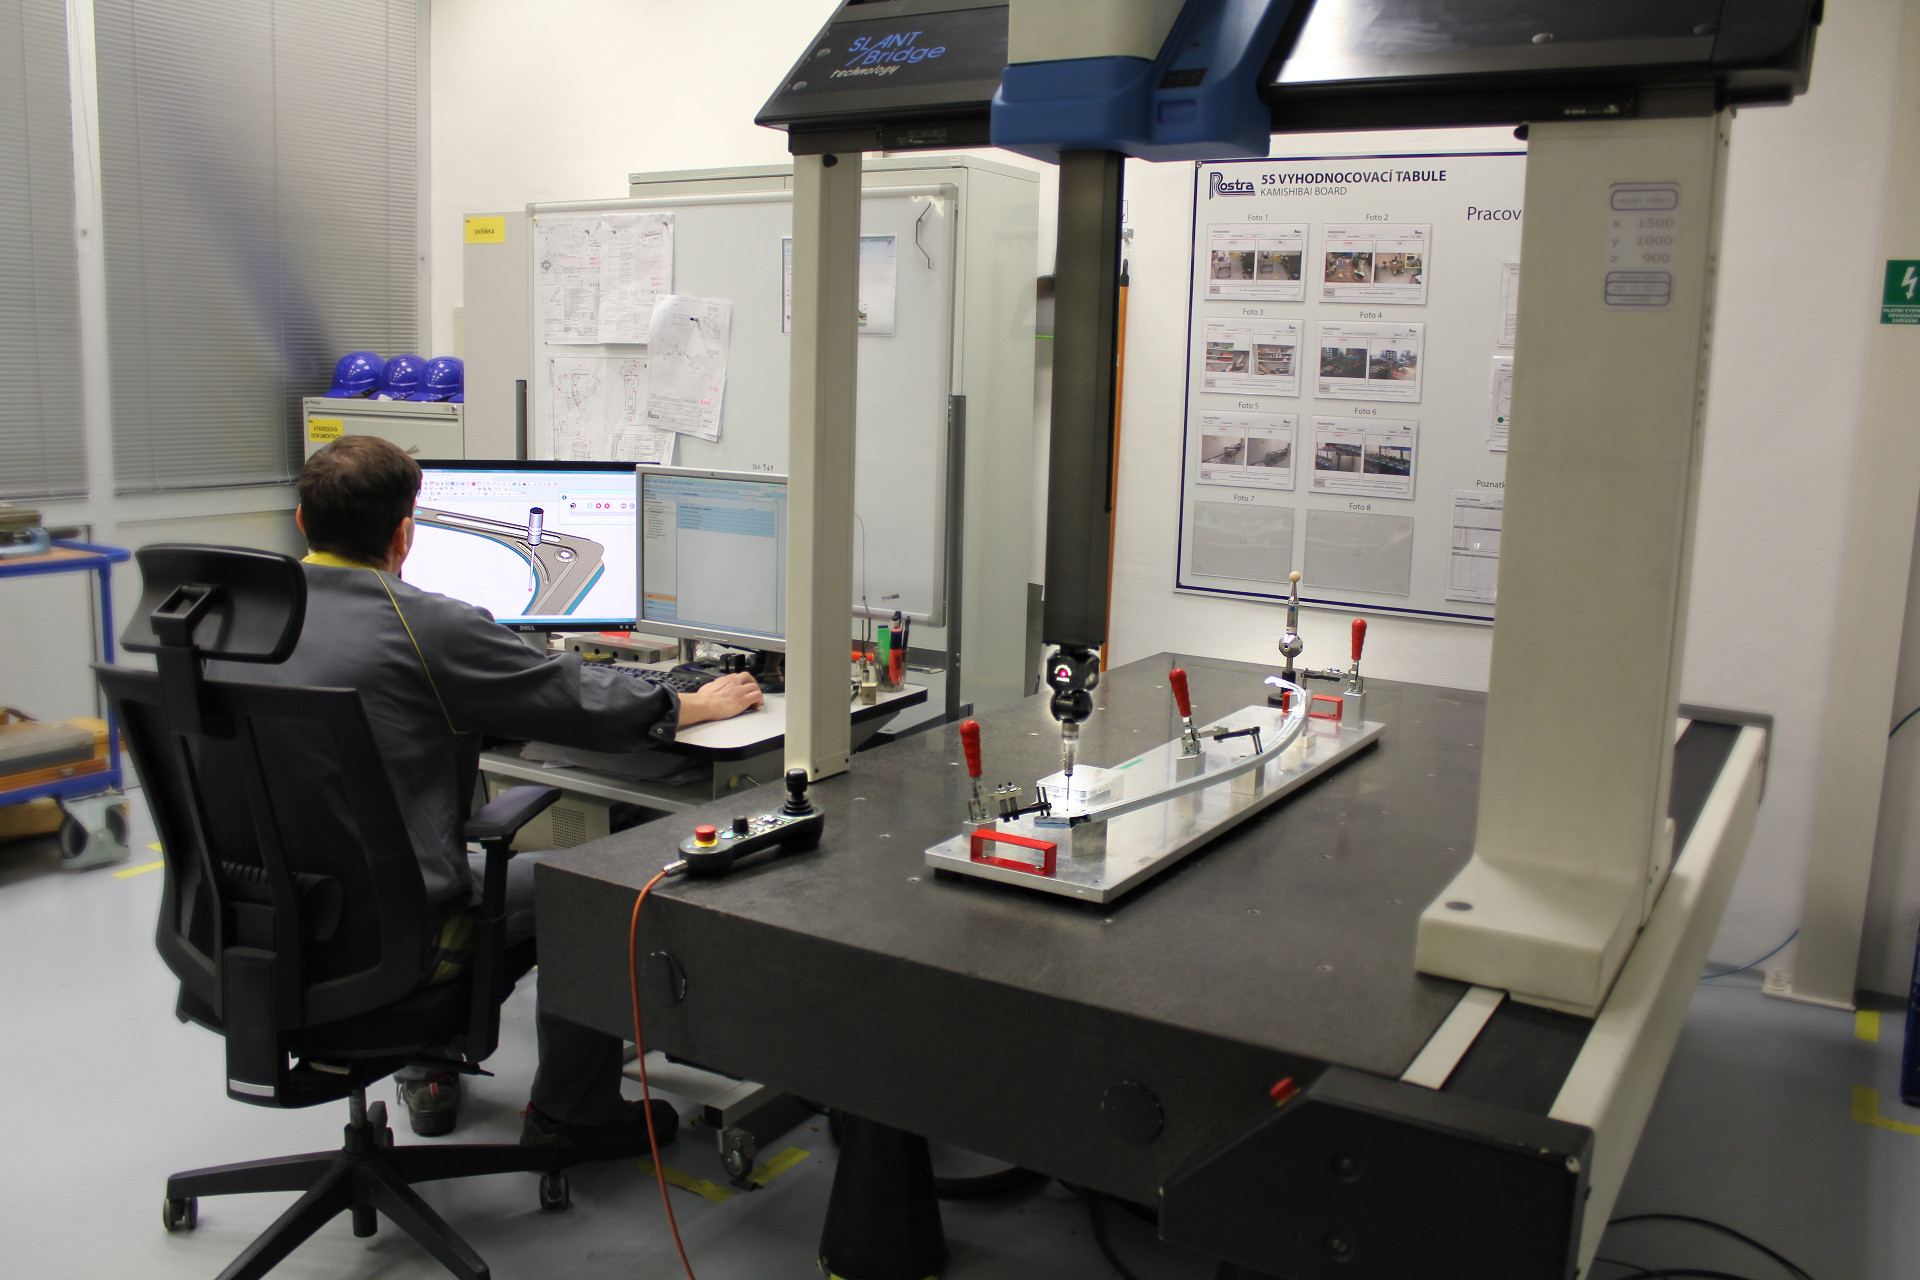
Inspection and production fixtures
We build inspection fixtures for checking the dimensions and geometry of parts and assemblies.
We also build assembly and welding fixtures to customer requirements.


A good tool starts with a well-thought-out design
The ROSTRA Tools design department designs press tools and moulds with an emphasis on the customer's technical requirements, reliable function and the efficiency of subsequent production.
In the design we take into account the shape and properties of the part, the chosen technology, material utilisation and tool life requirements.
3D design and CAD/CAM
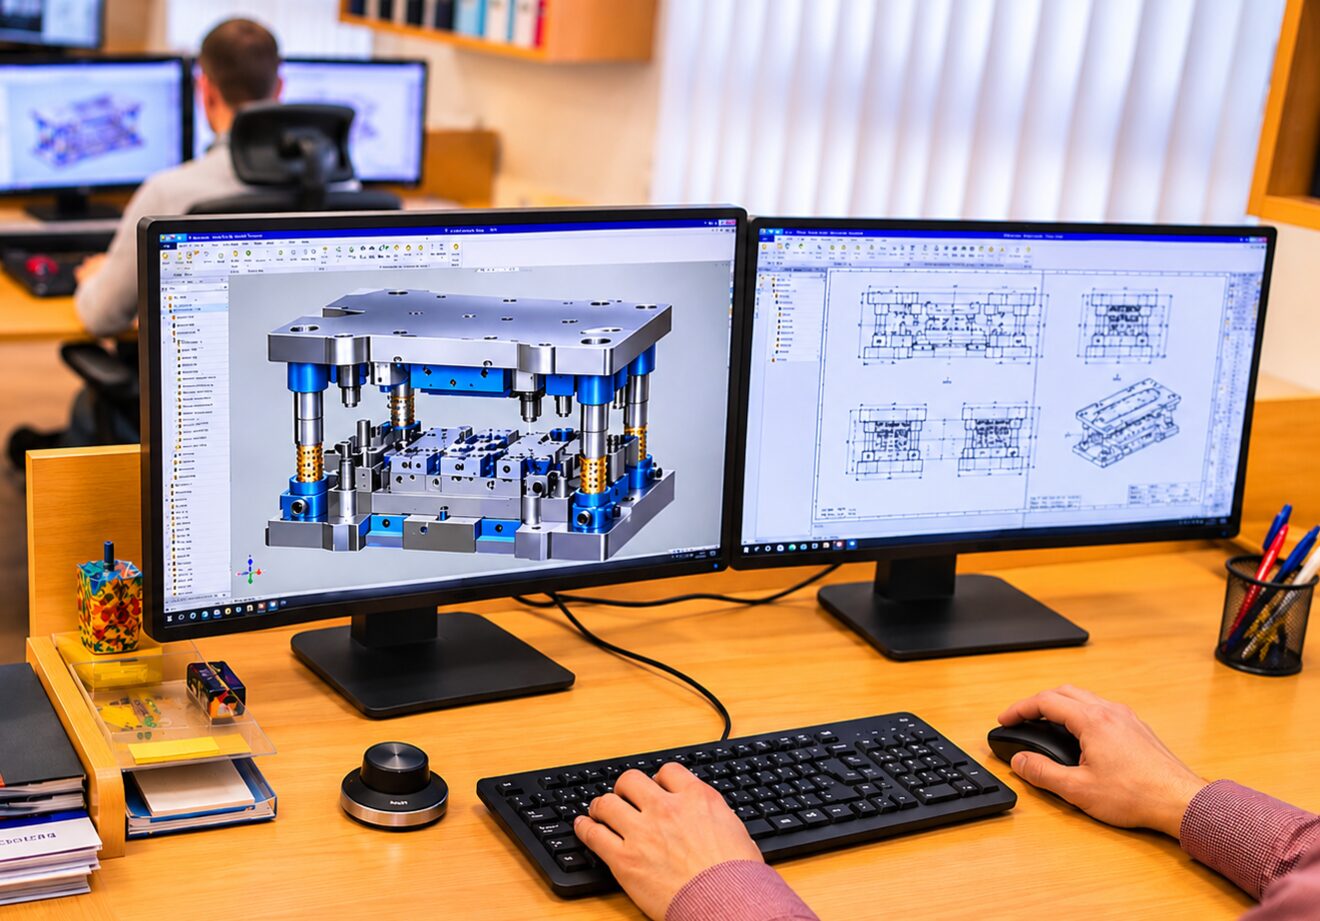
For design and production preparation we use Siemens NX and SolidWorks. 3D models allow detailed preparation of the individual tool components and how they fit together.
Stamping simulation
Stamping process simulations are carried out in cooperation with external specialists. We use their results to verify the proposed solution and make any design adjustments before production starts.
Digitalisation of production documentation
We have introduced drawing-less production. Digital 3D models make it easier to pass technical information between design, process engineering and production.
Modern technology for precision manufacturing
ROSTRA Tools has the technological equipment to produce press tools, injection moulds, precision machined parts and fixtures.
We combine CNC machining, EDM technologies and grinding. We choose the individual production processes according to the required precision, the part geometry and the technological demands of the job.
- 5-axis CNC milling
- We use five-axis machining to produce complex-shaped parts and press tool components. HERMLE machining centres allow precise machining of complex surfaces. Palletising on one of the centres supports automated operation.
- 3-axis CNC milling
- We use three-axis machining centres to produce larger tool parts, base plates and other precision machine components.
- Wire electrical discharge machining
- Wire EDM enables precise machining of conductive materials and complex contours. Selected machines are equipped with automated workpiece handling.
- EDM die sinking
- We use die-sinking EDM to machine complex cavities and details that are difficult to produce by conventional cutting.
- Precision grinding
- Surface and cylindrical grinding is used to finish functional surfaces and tool components that require precise dimensions and surface quality.


Technical capabilities and capacities
Complete machine park and working ranges
5-axis CNC machining centres 2 machines
Palletising on the HERMLE C32 centre lets the operator prepare a batch of clamped workpieces for a whole week — the machine picks up the next piece by itself and machines it.
| Machine | Model | X | Y | Z |
|---|---|---|---|---|
| HERMLE (with palletising) | C 32 | 650 | 650 | 500 |
| HERMLE | C 42 U | 800 | 800 | 550 |
3-axis CNC machining centres 5 machines
| Machine | Model | X | Y | Z |
|---|---|---|---|---|
| DECKEL MAHO | DMC 125P hi-dyn TNC 426 | 1220 | 880 | 800 |
| DECKEL MAHO | DMC 100V hi-dyn TNC 426 | 1000 | 880 | 500 |
| DECKEL MAHO | DMU 60T TNC 530 | 630 | 560 | 560 |
| TAJMAC–ZPS | MCFV 1060 Standard | 1016 | 610 | 760 |
| TAJMAC–ZPS | MCFV 1060 Standard | 1016 | 610 | 760 |
Wire EDM machines 5 machines
Machines with palletising run unattended overnight and at weekends — the automatic loader takes the next workpiece from the magazine as soon as the previous one is finished.
| Machine | Note | X | Y | Z |
|---|---|---|---|---|
| 2× FANUC RC C600iB | with EROWA palletising | 400 | 500 | 440 |
| FANUC α-C600iA | — | 1050 | 820 | 310 |
| FANUC α-C600iA | — | 1050 | 820 | 310 |
| FANUC α-1iD CE | — | 600 | 400 | 310 |
Die-sinking EDM 1 machine
Our EDM cell machines shapes that cannot be milled — tiny electrical discharges in a dielectric let us machine even very hard materials with a high-quality surface and high precision.
| Machine | Model | X | Y | Z |
|---|---|---|---|---|
| DECKEL | DE 25 C Multiform 4 | 500 | 350 | 350 |
Grinding 6 machines
| Surface grinders | Model | X | Y |
|---|---|---|---|
| ZIERCH GmbH | ZT 612, horizontal surface | 1200 | 700 |
| AQUASTYL SLOVAKIA | BRH AQ500, horizontal surface | 1000 | 500 |
| ZVL | BRH 20.05, horizontal surface | 630 | 230 |
| ZVL | BRH 20.02, horizontal surface | 630 | 230 |
| ZVL | BRH 20 NC, vodorovná rovinná | — | — |
| Cylindrical grinders | Model | Ø | L |
|---|---|---|---|
| TOS | BU 16, universal | 160 | 320 |
Tool assembly
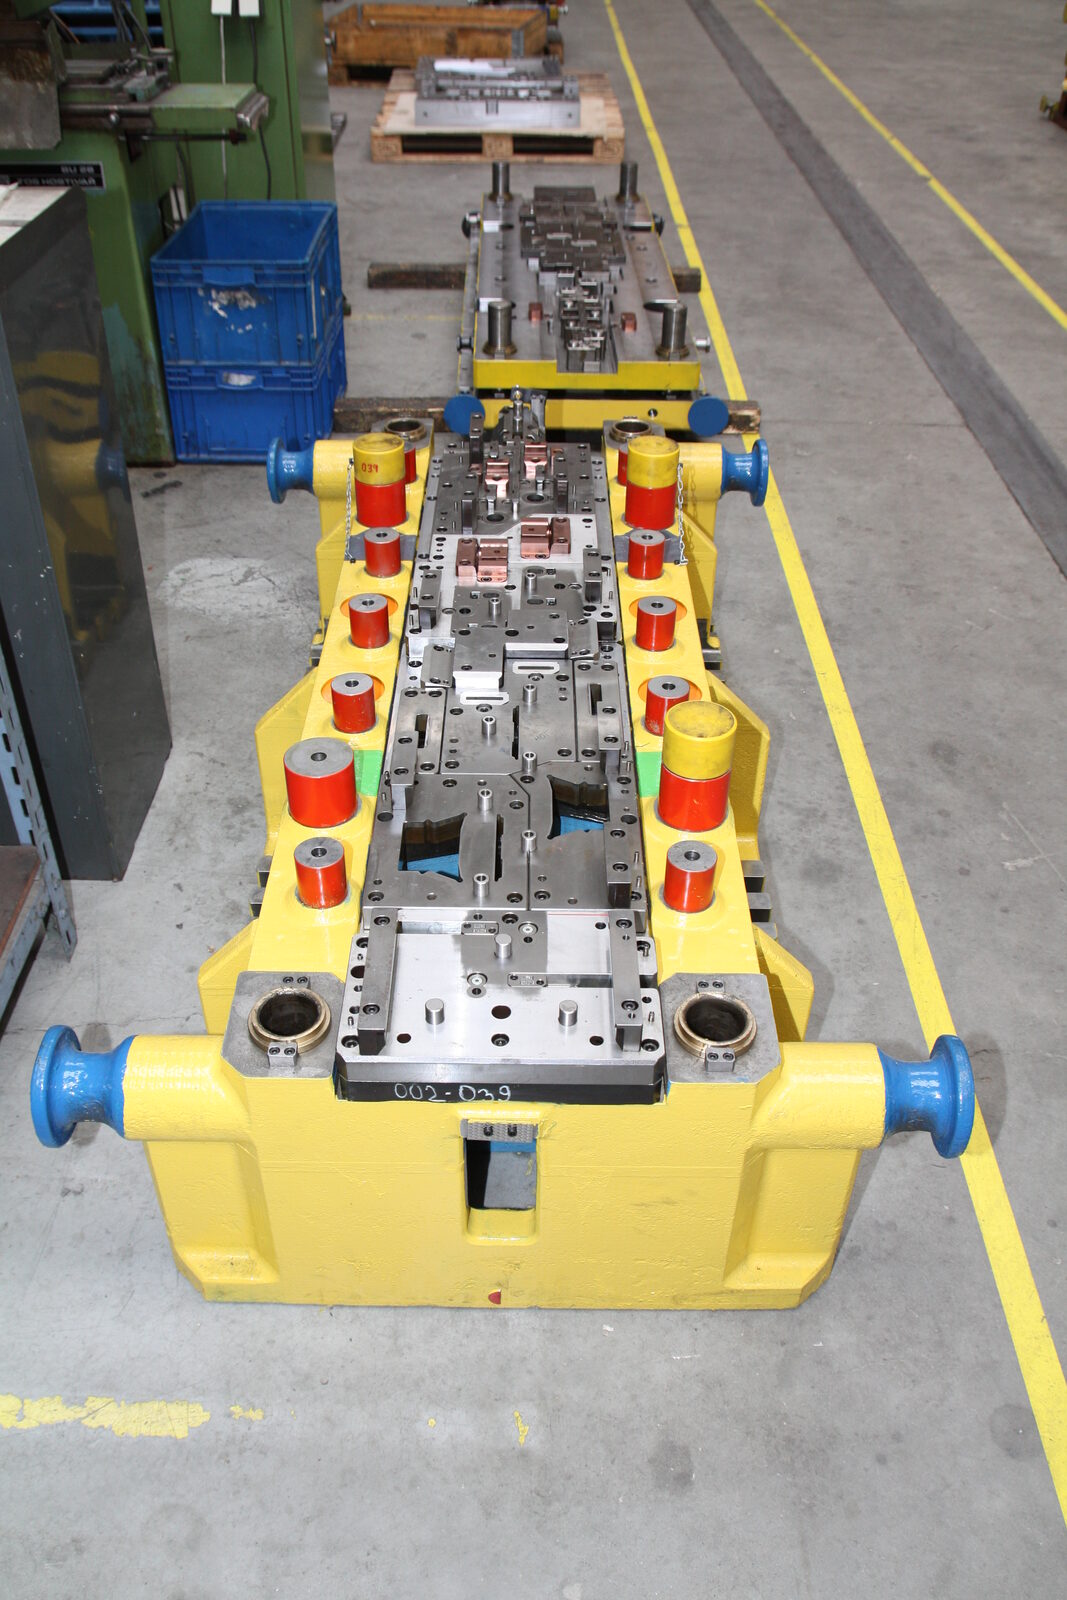
Maximum tool length 5 000 mm, maximum weight 30 t. Tool try-out before release to series production takes place in our sister press shop, ROSTRA Stamping.
We don't have a suitable machine? We can still offer you a solution.
In addition to our own production capacity, we also use external manufacturing subcontractors. If your workpiece exceeds the capabilities of our machinery or requires a different technology, we will check whether it can be produced in cooperation with our suppliers.
Actual manufacturability depends on dimensions, weight, clamping method, the required technology and other technical conditions.
Send us a drawing or 3D model. We will assess the technical feasibility and the approach individually.
Send a technical enquiryHow a press tool is made at ROSTRA Tools
Making a press tool involves a series of linked activities – from design preparation and machining of the individual components to assembly and functional verification.
Every project has its own technical requirements. We therefore adapt the individual steps to the tool design, the complexity of the part and the customer's requirements.
- 01
Design and simulation
We prepare the 3D tool design based on the technical specification. Depending on the project, we also use external stamping simulations and discuss the design solution with the customer.
- 02
Production preparation
Process engineers prepare the production routings for the individual tool components and define the sequence of operations and the required process methods.
- 03
Sourcing of materials and components
We source tool steels, standard components, guide elements and other components needed to manufacture and assemble the tool.
- 04
Manufacturing the individual components
We produce tool components using a combination of CNC machining, EDM technologies and precision grinding, according to their design and required parameters.
- 05
Tool assembly and try-out
We assemble the finished components into a functional unit. Toolmakers carry out fitting, adjustment and other finishing work needed for the tool to function correctly.
- 06
Try-out and hand-over
Depending on project requirements, we verify the tool's function during trial stamping, with the option of using the press equipment of our sister company ROSTRA Stamping.
Based on the test results, we make the necessary adjustments. We then hand the tool over to the customer with the agreed documentation.
We verify precision throughout production
Checking dimensions, geometry and functional properties is an important part of manufacturing press tools, moulds and precision machined parts.
We carry out inspections at each stage of production according to the technical documentation and the customer's requirements. Alongside 3D coordinate measurement we use modern optical technologies that help us identify geometric deviations faster and make targeted adjustments to tool components.

Optical 3D scanning
The AI-assisted KEYENCE optical 3D scanner enables non-contact digitisation of complex shapes and detailed comparison of actual parts with CAD models.
Colour deviation maps clearly show where the part geometry differs from the required shape. We use the measurement results for component inspection, tool optimisation and tool try-out.
The technology also makes it possible to digitise existing parts without original drawings. The data obtained can be used for design analyses, proposed modifications or the preparation of replacement components.
3D coordinate measurement
Coordinate measuring machines allow us to verify the dimensions and spatial geometry of the components we produce. A portable measuring arm can also be used to inspect selected parts and assemblies.
Inspection of details and surfaces
Pro kontrolu drobných geometrických prvků, rozměrů a vlastností povrchu využíváme optická měřidla, mikroskop, výškoměry a další specializovaná zařízení.
Inspection documentation
We adapt the scope of measurement and the output documentation to the project's technical requirements and the conditions agreed with the customer.
View overview of measuring equipment
DEA Global
DEA Mistral
Wenzel RS1215
Romer Absolute Arm 7525SI
Easyscope VID 3D MAN
Tesa Micro-Hite 600
Dia Vite DH-5
Škoda PB 1
SWI-100
VL-800 Keyence
MVD
ZD 10-90
Q2 ION
Also: magnetic particle inspection of safety parts and complete measurement documentation on the customer's request.


Experience from the automotive industry and other sectors
Our press tools and injection moulds are used in projects of leading automotive suppliers. We also apply our experience in tool design and manufacture in other industries.
Press tools for automotive
Our projects include press tools for specific automotive projects:
- BMW PL6/F07 – a project for Benteler.
- Daimler Staukasten – a project for Magna, intended for Mercedes-Benz Actros vehicles.
- PSA T75 – press tools built for the automotive industry.
- Audi, SEAT and Volkswagen – other projects to which we contributed by building press tools.
Injection moulds
Besides press tools, we also build injection moulds for plastic components.
Our references include, for example, moulds for the parts VW BULB-CAP a VW FTI-HOLDER.
Tools for racking systems
Our experience is also applied outside the automotive industry.
In recent years we have been making press tools for components of racking systems used in large logistics centres.
These projects involve large parts with requirements for precise geometry and mechanical strength. When designing the tools, we therefore consider not only the production technology but also the functional requirements of the final parts.
From toolmaking to series stamping
ROSTRA Tools and ROSTRA Stamping are two specialised companies of the ROSTRA group that operate on a shared production site in Vizovice.
This link allows us to offer customers two ways of working with us – stand-alone design and manufacture of a press tool, or tool manufacture followed by series stamping of sheet-metal parts.


- Tool try-out under real conditions
- Depending on the tool type and the technical capabilities of the press shop, we can use ROSTRA Stamping's presses for its try-out. The test results serve to verify functionality and to make any design or process adjustments before hand-over to the customer.
- Tool maintenance in series production
ROSTRA Tools provides repairs, maintenance and technical modifications of the press tools used at ROSTRA Stamping.
We use the experience from their day-to-day operation to optimise tools and design new solutions.
- Production experience fed back into design
- Close cooperation between the tool shop and the press shop allows lessons from series production to be passed directly to designers and process engineers. As a result, we can also take practical experience of tool use into account in new projects.
How working with ROSTRA Tools works
Do you have a drawing, 3D model or technical specification ready? Send us your requirements. We will assess the technical feasibility and prepare a quotation suited to the nature of your project.
- 01
Sending your enquiry
Send us a drawing, 3D model or technical specification of the required product or tool.
- 02
Technical feasibility assessment
We review the technical requirements, the feasibility of in-house production and, where appropriate, the use of external subcontractors.
- 03
Preparing the quotation
Based on the technical assessment, we prepare a quotation including the expected delivery date.
- 04
Agreeing the next steps
Once the quotation is accepted, we jointly finalise the technical conditions, the schedule and the next steps of the order.
The time needed to prepare a quotation depends on the complexity of the project and the completeness of the documents supplied.
Do you have your technical documents ready?
Send a no-obligation enquiryContact the sales department
E-mail: rostra@rostra.czPhone: +420 577 004 511